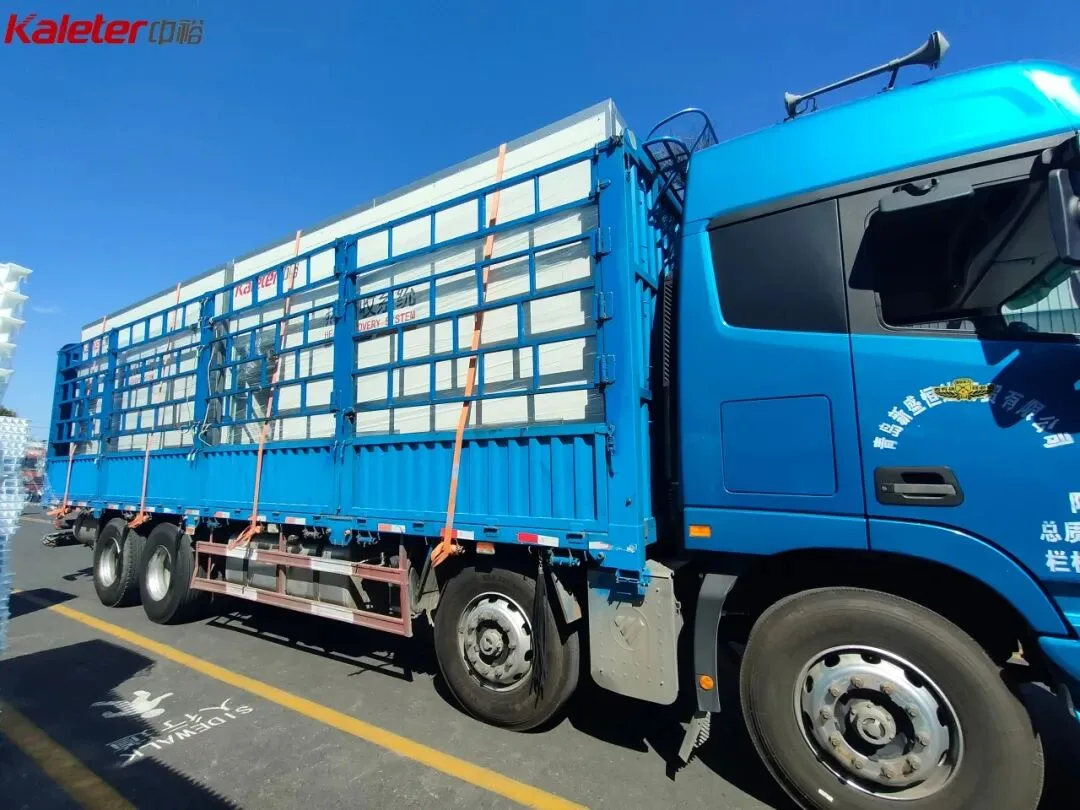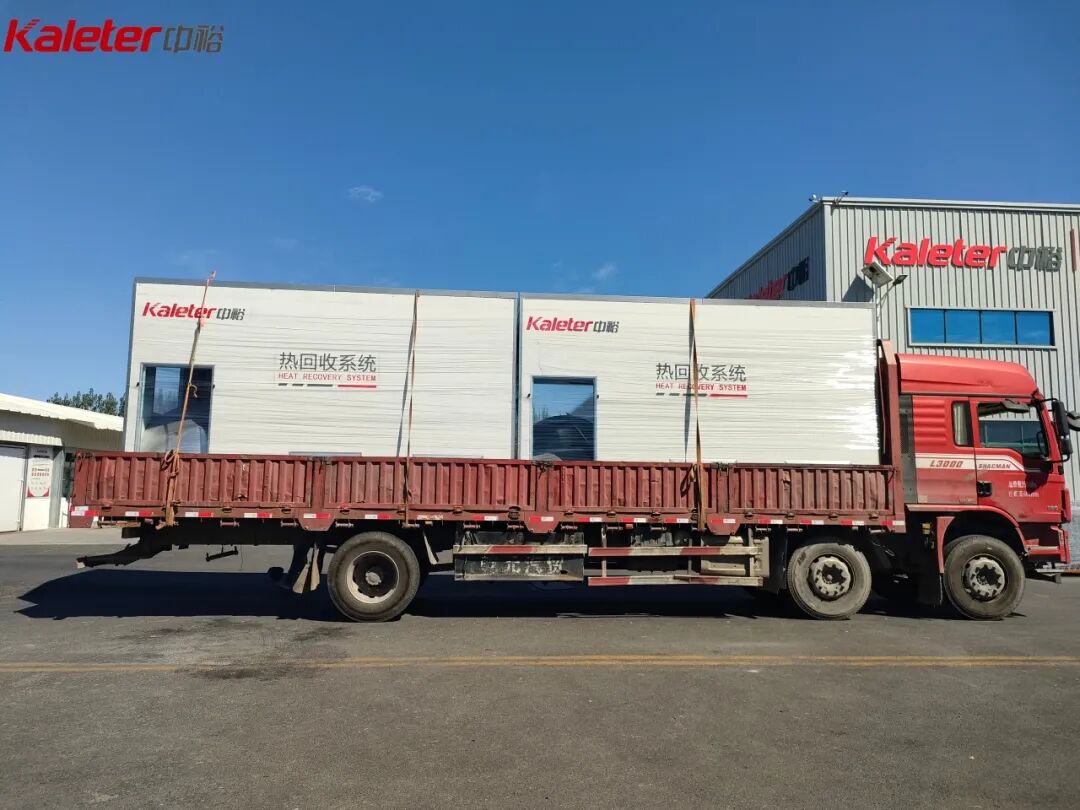
Kaleter recently finished production, commissioning, and quality inspection on several custom heat recovery units. The units are now loaded and on their way to the customer's site to support an efficient, high-quality installation. From precision manufacturing to strict testing, and from careful packing to secure loading, every step reflects Kaleter's attention to detail. The company delivers on its commitments and stands behind the quality of every project.
Heat Recovery Explained
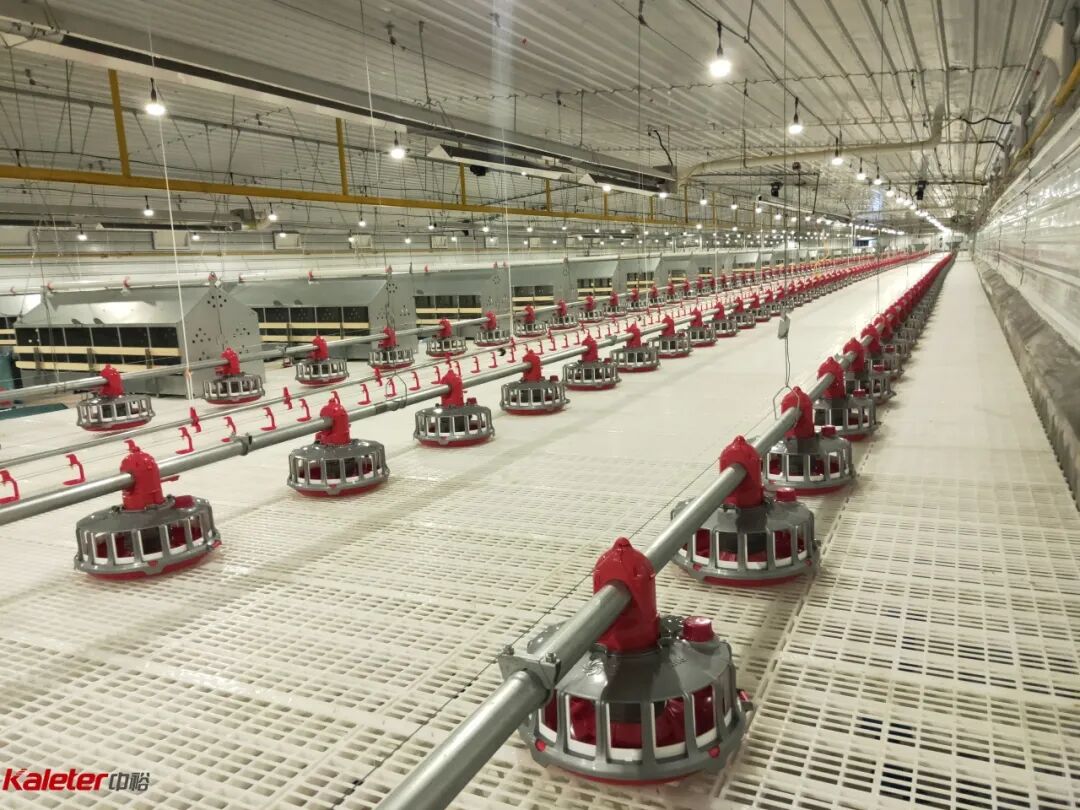
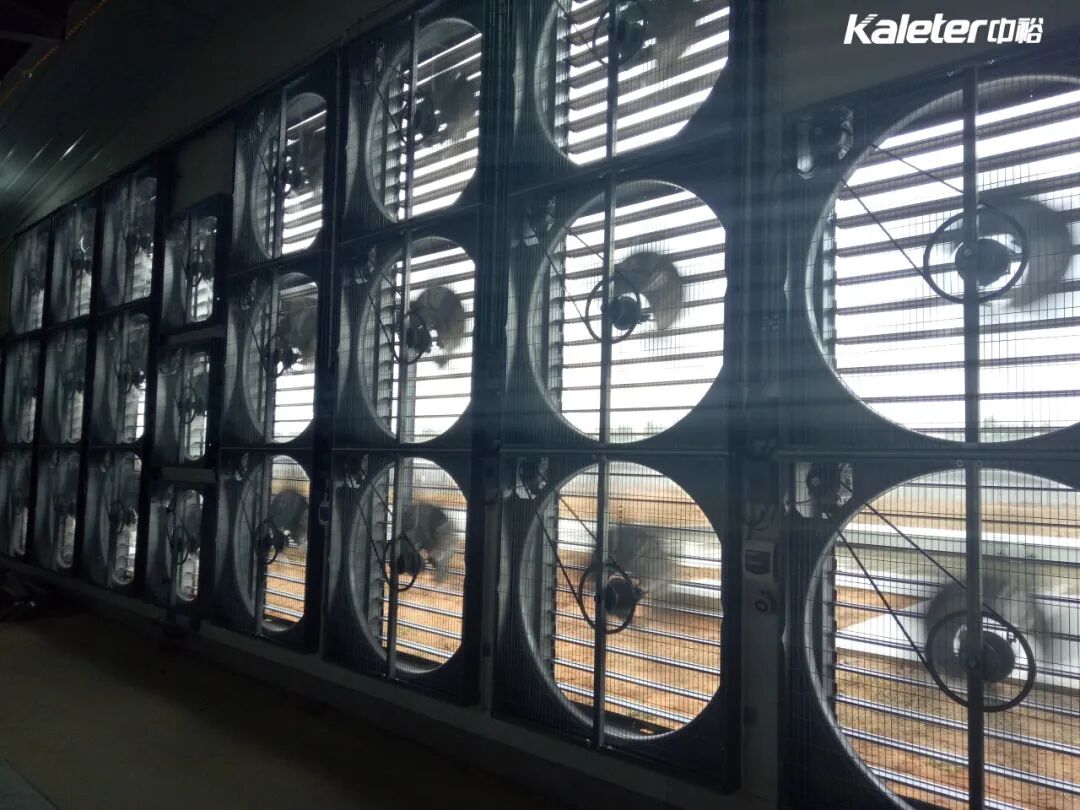
Kaleter's heat recovery environmental control equipment is built for large-scale poultry housing. It solves a problem the industry has long struggled with: ventilation and heat retention usually work against each other. The system removes stale, polluted air from inside the house and cleans the air the birds breathe, while recovering waste heat to preheat the incoming fresh air.
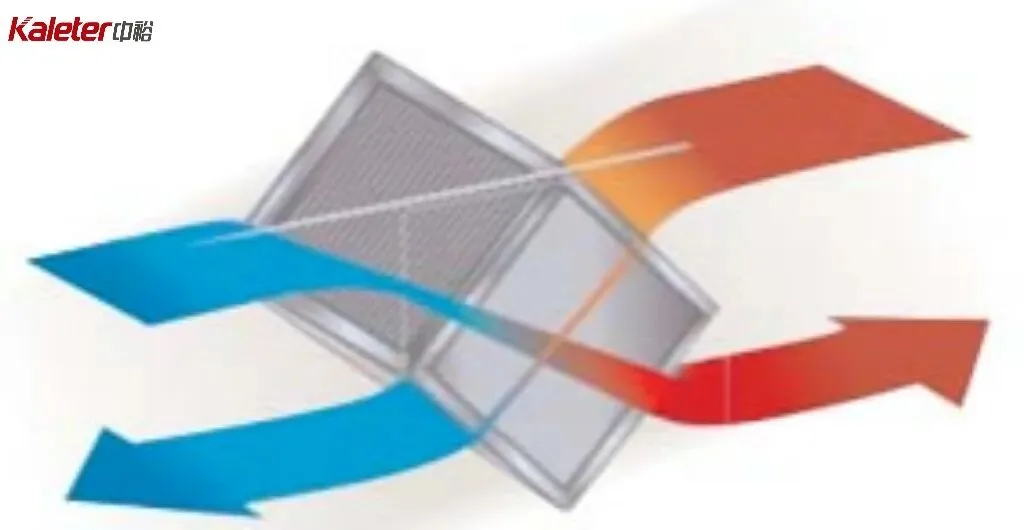
This keeps the house properly ventilated and protects the birds' growing environment. At the same time, it cuts winter heating energy use significantly and reduces cold stress on the flock. The system runs automatically and stays stable, helping farms lower energy costs and operate more efficiently.